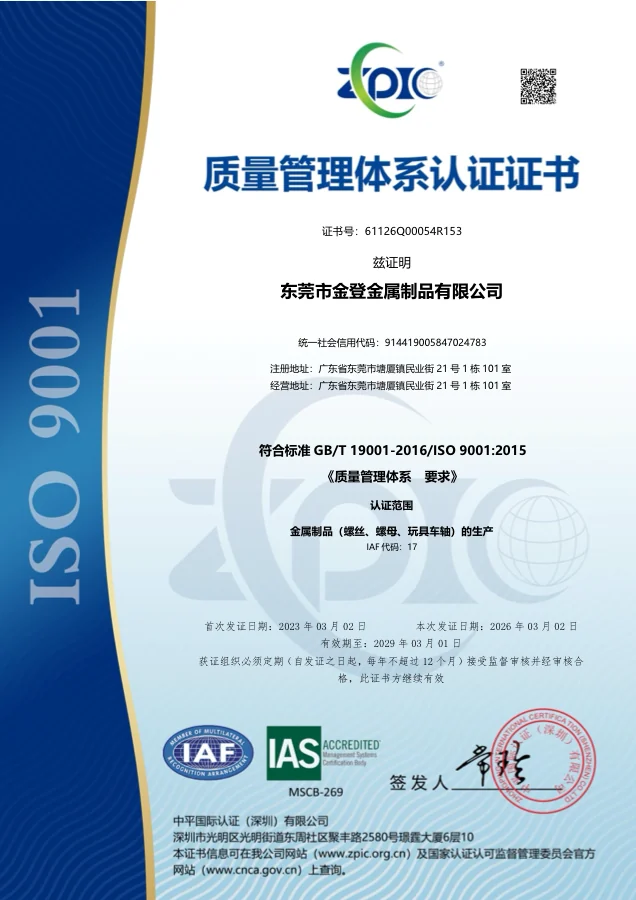
ISO 9001:2015
- No.
- 61126Q00054R153
- Issued by
- ZPIC (中平国际认证)
- Valid to
- 01 Mar 2029
- Scope
- Screws, nuts, toy axles · IAF 17
Cold heading, secondary machining and inspection under one roof — so a part is designed for the process, not forced into it.
Process
Not every part is cold-headed. The drawing decides the machine — a standard screw runs on an ordinary header, a complex shape moves to multi-station heading, and a tight-tolerance or low-volume part is turned. What follows is the same route either way.
| Stage | What happens |
|---|---|
| 1. Drawing review | We check the part against the process that fits it — head-to-shank ratio, tolerance stack, thread run-out. If a design change removes a machining step, we say so before tooling. |
| 2. Forming | The routing decision, then the machine: an ordinary header for standard screws, multi-station cold heading for complex heads and stepped parts, or automatic lathes where heading cannot hold the tolerance. |
| 3. Thread rolling | Threads are rolled, not cut. The grain follows the thread profile instead of being severed, which is why rolled threads hold higher stripping torque. |
| 4. Surface treatment | Zinc, zinc-nickel, nickel, blackening and passivation — barrel plating for small parts, rack plating where the finish has to stay unmarked. Every finish is quoted with a salt spray requirement (hours to red rust), so the coating is chosen against the environment rather than by name. High-strength parts are baked after plating to avoid hydrogen embrittlement. |
| 5. Heat treatment | Where the part needs property class 8.8 – 12.9, or case depth on a self-drilling point, hardening happens before plating and after forming. |
| 6. Inspection | Dimensional check against the drawing, plus salt spray, torque, hardness and 2D projection as the part requires. High-volume micro parts are optically sorted. |
| 7. Packing | Bulk, bagged or kitted to your line-side requirement, with the packing list checked against the order before the carton is sealed. |
| 8. Shipping | Pallets built at our own gate, export documents prepared for EU and US customs, material and coating certificates enclosed. |
On the floor
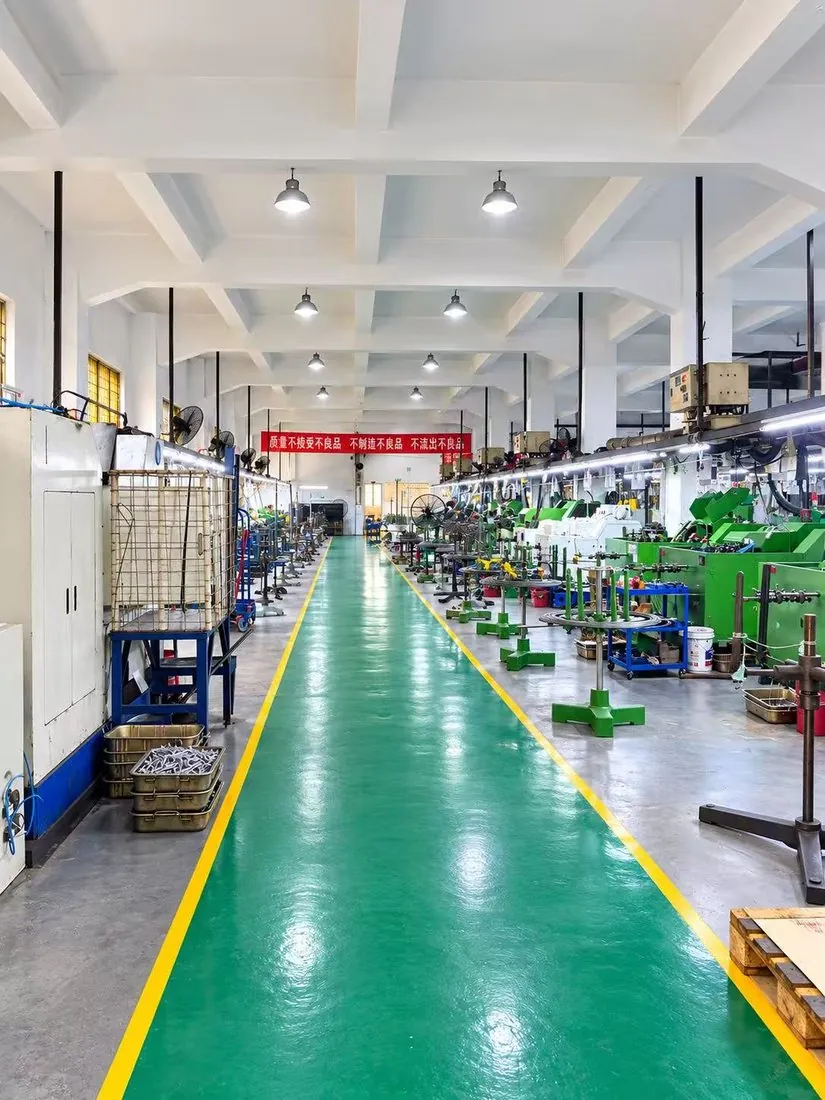
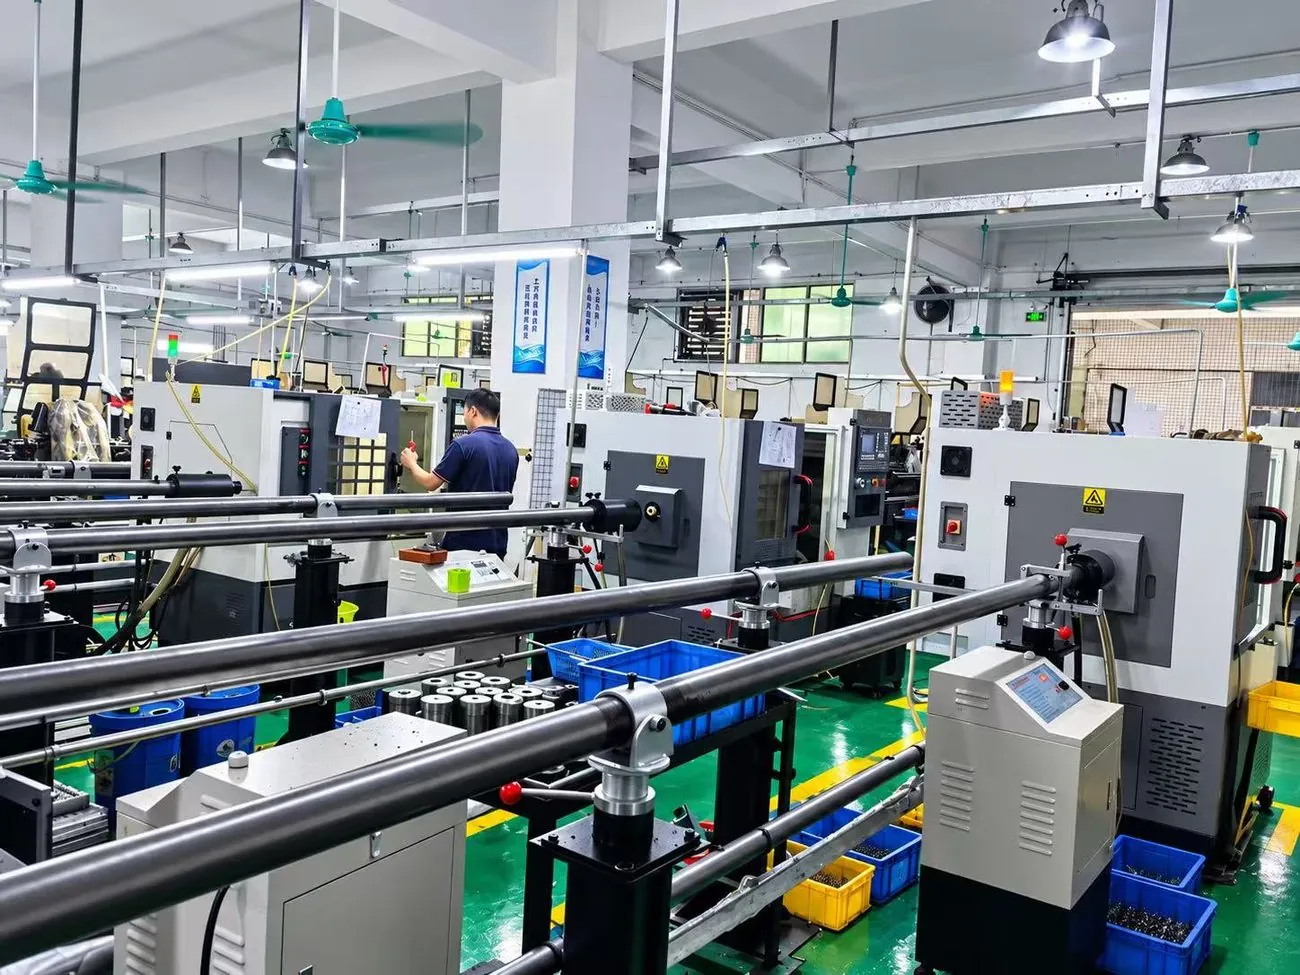
Cold heading and turning sit under the same roof. That is why we can recommend the cheaper route for your part instead of the one that keeps our own machines busy.
Product families
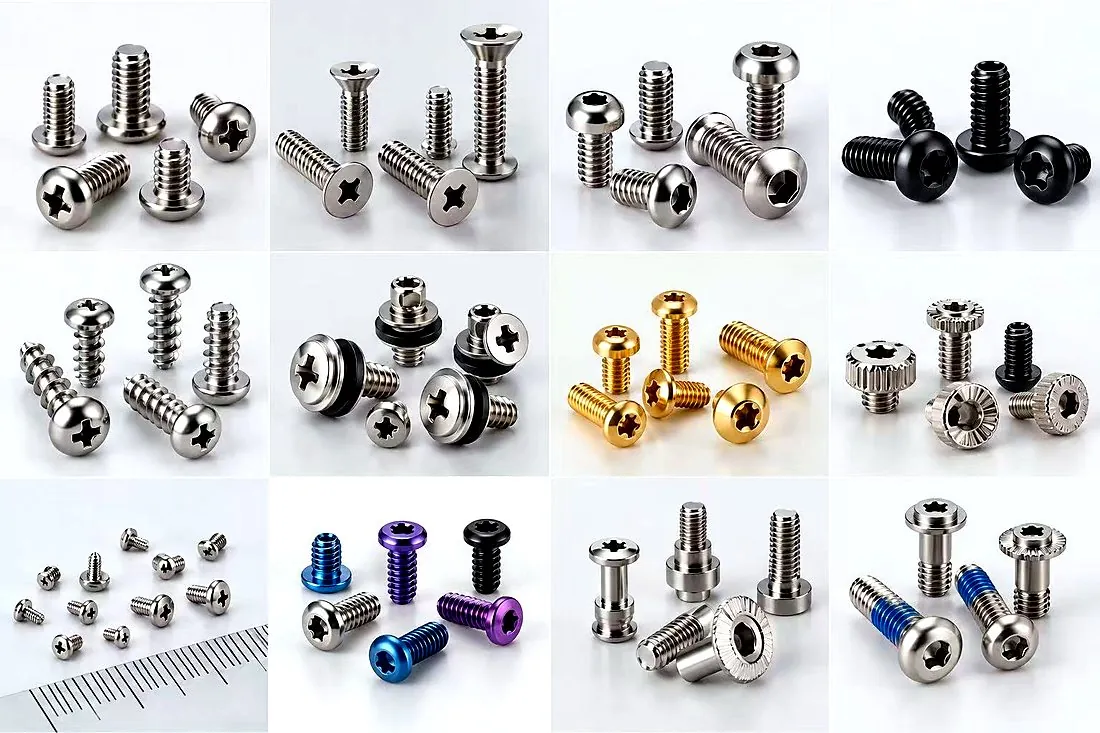
A single programme often pulls from five or six of these at once — which is what makes a complete fastener package possible from one purchase order.
Shoulder held by the die, repeatable across batches without secondary turning.
Washer and lock features assembled in-line; coloured heads for visual inspection.
Slotted and cross-recess drives for hand and automated assembly.
Non-standard drive recesses for tamper-resistant assemblies.
Thread-locking features and preload control for vibration-prone joints.
Spring-loaded assemblies for contact and take-up applications.
Point geometry and case depth for sheet metal and plastics.
Fluted, eccentric and other shapes that have no catalogue number.
Turned from bar where heading cannot hold the tolerance.
Turned nuts and inserts, including thin-wall and non-standard threads.
Knobs, housings and light structural parts, turned from bar on our lathes.
Contacts and conductive pins turned from bar, including charging connector parts.
Aluminium and copper parts are turned on the same lathes that back up our heading lines, so a programme does not need a second supplier for the machined pieces.
Materials & finishes
| Carbon steel | 4.8 – 12.9, with heat treatment where required |
| Alloy steel | For high-strength and fatigue-critical parts |
| Stainless steel | 304 / 316, including parts for wet and food-contact environments |
| Aluminium | CNC knobs, housings and light structural parts |
| Copper alloys | Contacts and conductive parts |
| Finishes | Zinc plating, nickel plating, blackening, passivation, natural |
Quality
Coating durability checked to the hours your specification calls for.
Wet and outdoor use · e-bike · cleaning equipment
Drive and stripping torque for structural and assembly-critical parts.
Robot joints · EV brackets · motor mounts
Profile, step diameter and thread geometry verified against the drawing.
Step screws · caster pins · first-article reports
Case depth and core hardness on heat-treated batches.
8.8–12.9 parts · self-drilling screws
Measuring instruments run on a scheduled calibration cycle — certificates available on request.
See the quality certificates and test reports ↓
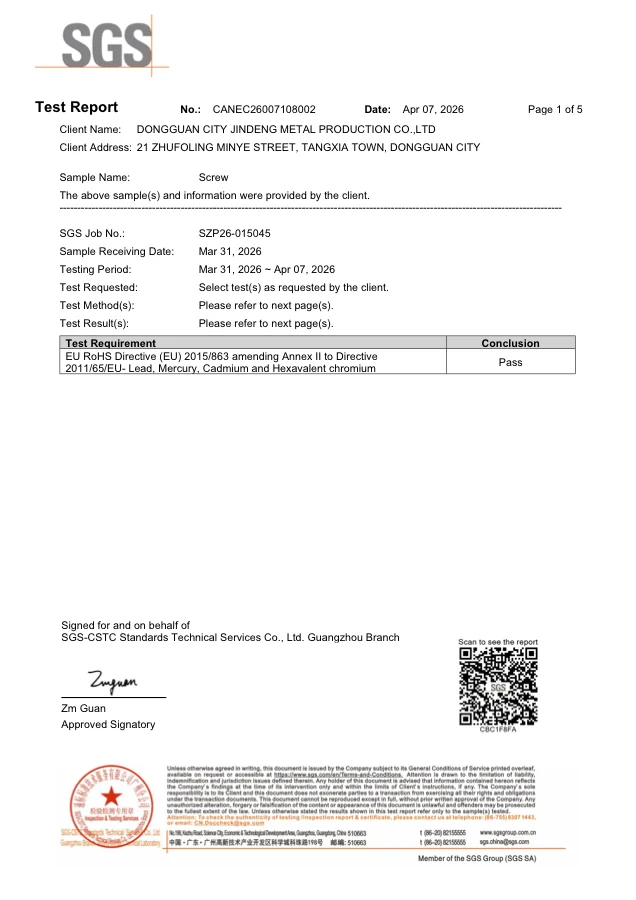
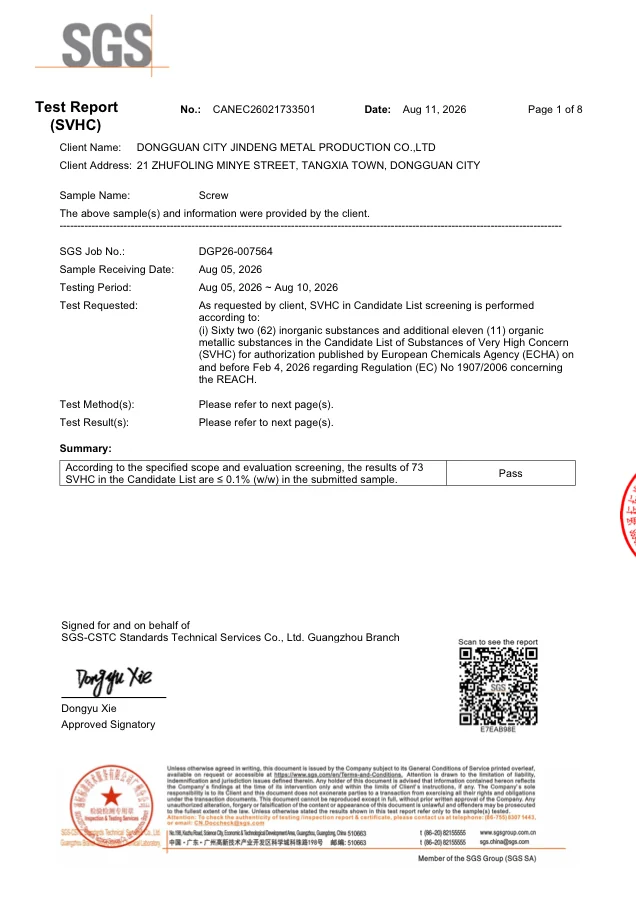
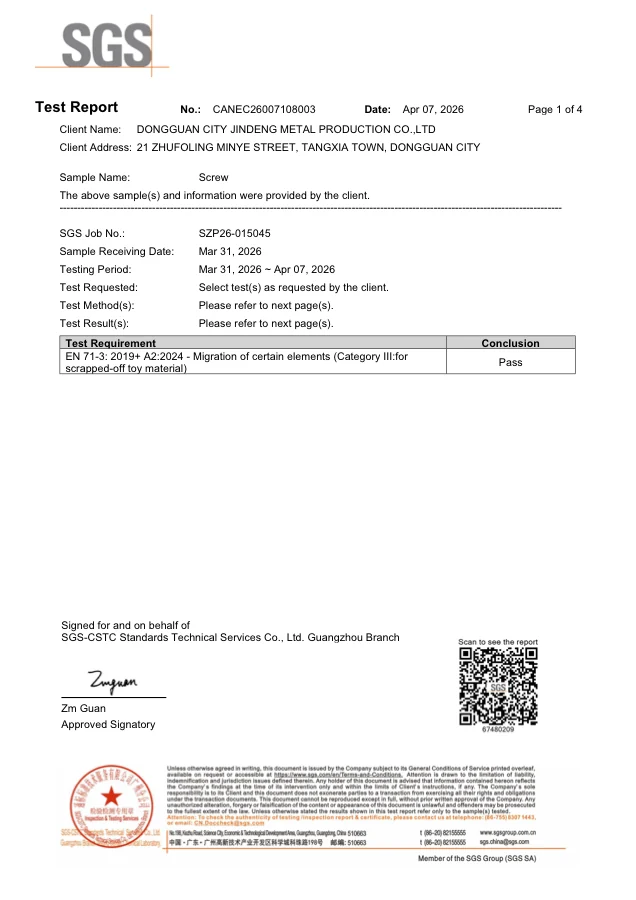
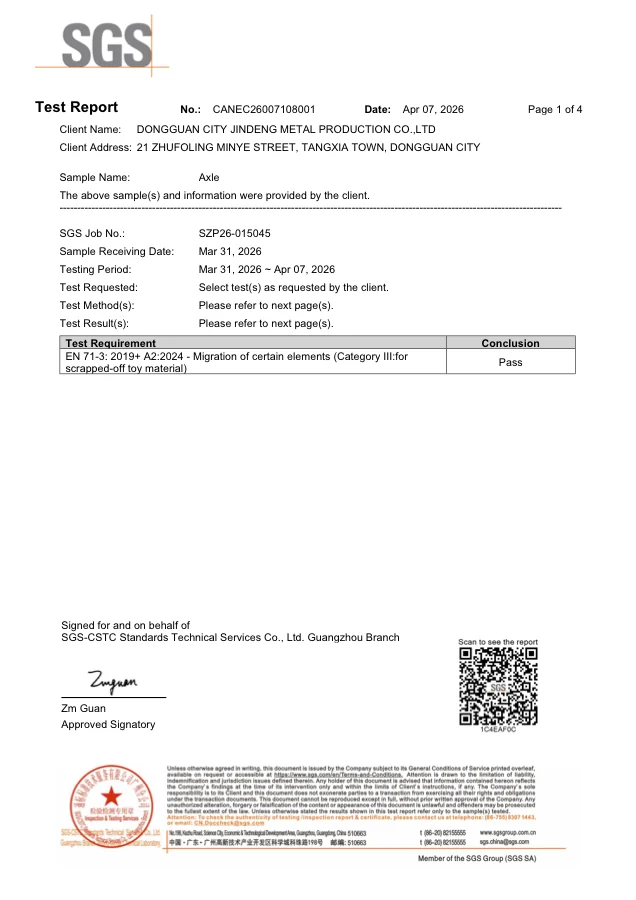
Certified to ISO 9001. Materials and finishes comply with RoHS; SGS reports and material certificates are supplied with samples on request.
The company
| Manufacturing since | 2005 — 21 years of fastener and hardware production |
| Exporting since | 2012 — 14 years supplying buyers in Europe, Latin America and the CIS |
| Plant | 4,500 m² in Tangxia Town, Dongguan — 100+ heading machines, 20+ imported multi-station presses, plus lathes and CNC |
| Tooling | 30,000+ existing dies, used to avoid new tooling charges wherever possible |
| Certification | ISO 9001 · RoHS compliant materials and finishes · SGS reports on request |
| Trade assurance | Alibaba Verified Supplier since 2014 |
Certificates
All current, all downloadable. The certificate numbers can be verified with the issuing body — we would rather you check them than take our word for it.
Send the drawing — we will tell you whether it can be cold-headed, and what it would cost.
Send a drawing